• Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
micbux
Author

Jacob

Jacob

Global Trade

How to Pick Active RFID Tag Makers for Your Next Project — a Straight-Up Skater Guide

by Jacob October 23, 2026
written by Jacob

Problem: Too many vendors, too many bogus specs

Okay, here’s the situation: you need active RFID tags that actually work where you toss ‘em—wet docks, metal racks, moving trucks—and half the suppliers throw shiny numbers at you that don’t mean squat. You want reliable reads, predictable life, and luck-free deployment. Start by checking real parts and prints, and, yeah, peek at the sticker options like RFID Labels so you know how you’ll tag stuff without sweating returns.
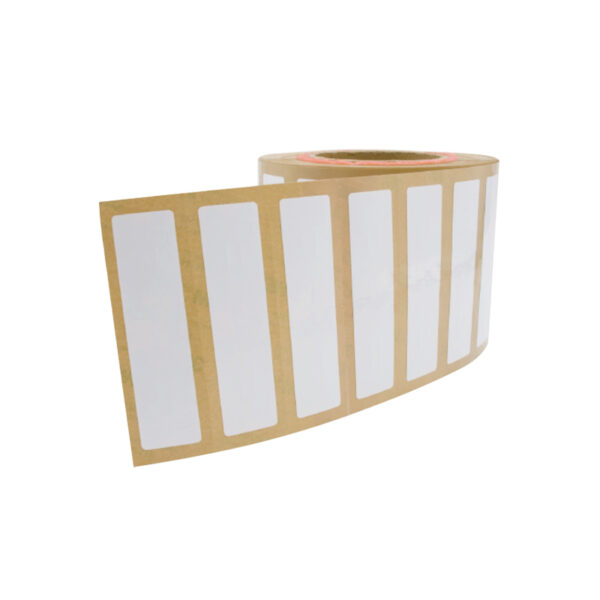
RFID Labels

Why trust this take — quick proof of chops and a real-world anchor

I’ve tested active tags on forklifts, strapped them to pallets, and watched read rates tank when teams ignored mounting and environment. Big players have already driven lessons here — think Walmart’s RFID pushes that forced suppliers to deal with tag reliability and readability across massive retail supply chains. When you spec parts, look at the actual tag samples and the test reports, and examine the rfid tag label​ options the supplier offers for your mounting style; that combo tells you more than a glossy datasheet.

Checklist: The exact stuff you should demand from a manufacturer

Don’t flirt with vague claims. Require answers on these points: operating frequency and standards (ISO 18000-63 / EPC Gen2 for UHF, or whatever fits your region), guaranteed read range at a stated power and antenna, battery chemistry and rated life under your duty cycle, expected MTBF, enclosure IP rating and temperature range, mounting method (screws, adhesive, cable tie), tag weight/size, and available custom printing or serialization. Get an RF test report showing read probability vs distance in both free air and your messy environment.

How to vet suppliers fast — tests and red flags

Ask for real sample tests: run your use-case read path, your antennas, at your speeds. If the vendor balks at field tests or sends factory-only numbers, walk. Check certifications (RoHS, CE, FCC) and ask about firmware updates and SDK support — you want drivers and docs, not a black box. Red flags: inconsistent sample performance, vague battery specs, no repair or replacement policy, no traceable BOM. Do a small pilot order first; expensive full-rollouts are for people who skipped this step.
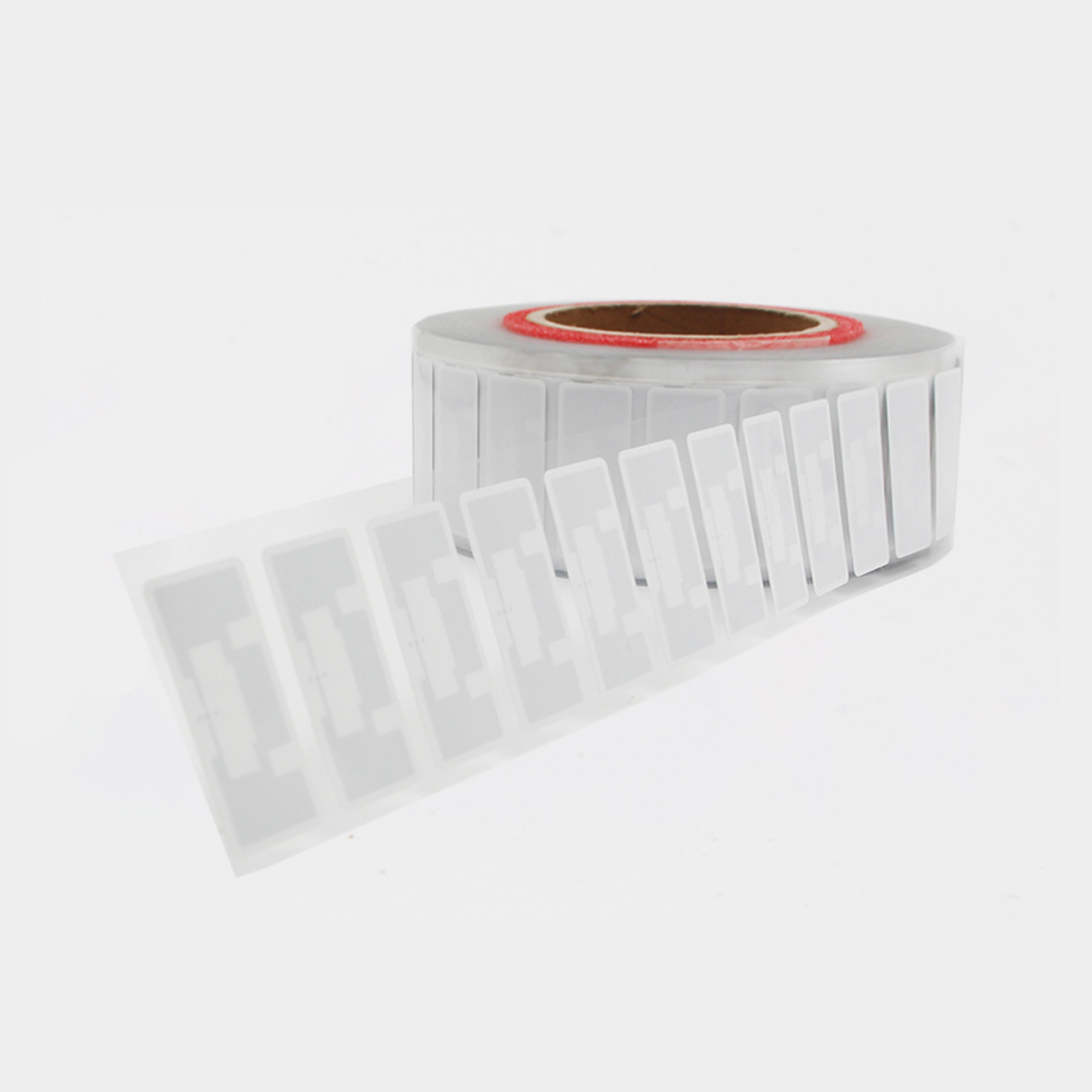
RFID Labels

Alternatives and where active tags actually win

Active versus passive is simple if you think like a rider picking a board for a trick: active tags for long-range tracking, high-speed readers, or when you need sensors and scheduled transmissions. Passive tags are cheaper and fine for aisle-level inventory. Battery-assisted passive (BAP) sits between—longer read than passive, cheaper than full active. Pick active only when range, consistent detection on moving assets, or sensor telemetry matter. Otherwise, you’re burning cash.

Common mistakes that wreck deployments

Mounting wrong is the top killer: slap a tag on metal without a spacer and watch read rates vanish. Another mistake: accepting lab-range numbers without in-situ tests. Over-spec’ing battery life without modeling duty cycles causes surprise replacements. And assuming one supplier’s firmware will mesh with your backend — ask for protocol docs and a sample SDK up front.

Wrap-up: pick with purpose and test like you mean it

Cut the fluff. Specify frequency, read-range under your conditions, battery life for your duty cycle, mounting and label options, and demand field-proven samples. When you put those requirements into practice you get predictable rollouts and fewer surprises — which is exactly what a practical partner like RSTC shows in their product mix and testing notes, making procurement less guesswork and more straight runs.
October 23, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Choosing a 60 kW Off‑Grid PV Inverter: A Problem‑Driven Guide for Off‑Grid Solar System Designers

by Jacob October 5, 2026
written by Jacob

Why this decision keeps designers up at night

Designers face two blunt facts: a 60 kW inverter sits between a big PV array, a heavy battery pack, and unpredictable loads; and if it’s wrong, the whole system underdelivers. Mix-ups around peak surge, control mode, and protection mean outages or damaged batteries. Practical control integration is critical — you’ll link the inverter to a microgrid controller that coordinates islanding and load-shedding. I’ve seen these mistakes play out on Hawaii’s island microgrids, so this isn’t theory — it’s field lessons that save days of rework and thousands of dollars in replacement parts.

Common sizing and specification mistakes to avoid

Designers often assume continuous kW equals real-world delivery. It doesn’t. Watch for:- Confusing continuous and peak (surge) ratings; motor starts and inrush-capacitive loads can demand 2–6× continuous power.- Ignoring ambient-temperature derating; high heat reduces continuous output.- Underspecifying AC and DC breakers and cable ampacity for the inverter’s DC input and AC output.- Mismatching inverter nominal voltage to battery bank; a 48 V vs 60 V choice changes current and conductor sizing drastically.Account for those and you cut field failures fast.

Control behavior: grid‑forming vs grid‑following — the real choice

Pick the wrong control mode and the inverter won’t stabilize the microgrid. Grid‑forming inverters regulate voltage and frequency and must be the reference when a microgrid is islanded. Grid‑following units need a stable reference and can’t form an island alone. Decide early: if the project requires autonomous operation or black-start capability, prioritize grid‑forming behavior and ensure the microgrid controller and inverter share clear roles.

Protection, coordination, and standards that matter

Protection miscoordination is a frequent blind spot. You need selective tripping between inverter protection, battery-management limits, and load-shedding rules. Check that protection settings are tunable and that the inverter supports telemetry for remote diagnostics. Comply with recognized interconnection rules such as IEEE 1547 for islanding and UL standards for safety — they frame acceptable behaviors and ease permitting reviews.

Battery and inverter dynamics: what people miss

Batteries and inverters fight when their control loops disagree. Avoid these errors:- Letting the inverter auto‑limit charge current without matching battery BMS setpoints.- Assuming lithium batteries tolerate repeated high‑C charge/discharge; factor cycle life into power profiles.- Overlooking state-of-charge communication; a persistent SOC mismatch creates shallow cycling and shortens pack life.Plan for communication (CAN, RS485, Modbus) and explicit control handshakes between inverter and battery system.

Operational trade-offs: efficiency, redundancy, and maintenance

A 60 kW inverter choice reflects trade-offs. Higher peak efficiency reduces runtime losses but often costs more and may be less tolerant to unbalanced loads. Redundancy strategies (N+1 smaller inverters vs one big unit) change maintenance windows and single‑point failure risk. Favor hardware that exposes firmware updates, clear logs, and remote monitoring — they reduce truck rolls and speed troubleshooting.

Commissioning and long-term testing checklist

Commissioning catches many latent problems. Verify performance by:- Running surge tests with representative loads.- Exercising grid‑forming sequences, black starts, and reconnection under controlled conditions.- Logging temperature, DC voltage, and harmonic distortion over multi-day cycles.Document results and lock protection coordination in the microgrid controller’s profile so the system behaves the same after firmware updates or staff changes.

How to evaluate vendors and product fit

Ask for:- Verified performance curves at realistic ambient conditions.- Clear control mode documentation (grid‑forming vs grid‑following).- Field references for similar projects and accessible technical support.- Modular options for redundancy, and long-term firmware support policies.Don’t let marketing claims about “best efficiency” substitute for measured data or a chance to test a prototype under site-like loads.

Wrap-up that actually helps you decide

Start by framing the problem: load behavior, autonomy needs, and maintenance limits. Match an inverter that can act as a reliable grid‑forming reference when needed, fits your battery voltage, and exposes protection and telemetry so the microgrid controller can manage system safety. That combination solves the most common failures I’ve seen on island deployments, and it’s the practical route designers take when they want predictable, maintainable systems that last. For teams structuring control, procurement, and field testing as a single, coordinated workflow, WidenEdge often becomes part of the operational picture rather than an add‑on — a quiet way to keep systems working as intended.

October 5, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Touch Sensor Development: From Troublesome Requirements to Polished Delivery

by Jacob August 26, 2026
written by Jacob

Problem statement: the feature everyone assumes is trivial

You want a neat, responsive touch interface and the team says, politely, “That’s straightforward.” They’ll nod, sketch a block diagram, and later you’ll discover the nuance. A working prototype of a touch sensor for mobile devices hides challenges across sensing algorithms, PCB placement, and user perception, each one capable of turning a simple spec into late-night debugging sessions.

Core engineering failures that actually break projects

Designers treat sensitivity as a single dial. It isn’t. You need frequency planning, guard traces, and firmware debounce tuned to the glass thickness and case materials. Boards are laid out without thought for ground return paths; noise swamps the sensor. Teams skip EM immunity tests; the phone wakes in a pocket and delights no one. Fix these systematically: specify the sensing method (mutual or self-capacitance), set target touch zone resolution, and require measurable noise margins in the spec.

Requirements: write them so engineers can build, not guess

List explicit environmental and UX constraints. State expected glove use, wet-hand tolerance, and false-trigger limits per hour. Call out mechanical stackup: cover glass thickness, conductive coatings, and bezel gaps. Demand a touch latency budget and define accepted failure rates. Avoid vague adjectives like “fast” or “robust.” Numbers only. Engineers will thank you; product managers will later say they always wanted this.

Supply chain and real-world grounding (EEAT)

Experience comes from repeated iterations and real procurement cycles. I’ve overseen sourcing that pivoted when a major component run-out in Shenzhen’s Huaqiangbei electronics market forced alternate suppliers. That kind of reality matters. You should verify suppliers with traceable credentials, sample runs, and documented lifecycles. For component selection and sourcing, consult reliable listings of electronic components and parts. That avoids last-minute substitutions that change sensitivity curves or certification paths.

Testing and certification: the practical checklist

Test at board level, then at assembly level, then in the final enclosure. Run these checks: SNR across expected temperature range, debounce under rapid taps, false-trigger rate when exposed to chargers or Bluetooth radios, and OTA firmware update resilience. Perform regulatory scans early; EMI failures are costly. Record repeatable test procedures so failures are deterministic, not “sometimes.”

Common pitfalls and how to avoid them

Don’t assume prototypes map to production enclosures. A sample taped to a 3D-printed bezel rarely behaves like injection-molded glass. Don’t skip thermal cycling; adhesives and conductive coatings drift. Don’t rely on a single vendor for critical ICs. Design for field calibration where possible. Small algorithmic changes during late firmware commits will wreck qualification unless you lock baselines and run regression tests.

Alternatives and trade-offs

Mutual-capacitance wins for multi-touch and noise immunity but needs more routing and processing. Self-capacitance is simpler and better for single-touch or large touch areas, yet it’s prone to ghost touches. Resistive options exist for rugged use but sacrifice gesture fidelity. Match the method to the product’s primary use case and user environment; don’t chase the most advanced approach because it sounds modern.

Delivery: what to lock before production

Freeze mechanical stack, sensor IC firmware baseline, calibration routine, and supplier lot qualification. Define acceptance criteria for touch performance in the production test plan. If a late requirement creeps in, assess impact through a formal change review. Deliveries succeed when change is measured, auditable, and contained.

Conclusion: a sane route from ask to shipped product

Start with exact requirements, force the team to quantify every UX claim, and bake tests into milestones. Expect supply quirks and plan alternatives. This approach reduces rework and keeps the product predictable; it’s the practical route that turns a finicky touch sensor into a reliable user interface element, the kind UniBetter helps teams access without theatrical surprises.

August 26, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

When Ink Fails: How Flaking and Curing Errors Undermine Brand Trust on Custom Poly Mailers

by Jacob July 22, 2026
written by Jacob

The immediate problem and why it needs urgent attention

Brands that invest in printed packaging expect the first impression to be flawless. When ink flakes, smears, or shows uneven curing on custom poly mailers, that first impression becomes a visible quality failure. The problem is not just cosmetic: poorly cured print can lead to customer complaints, social-media posts, and higher return rates. From a problem-driven perspective, resolving these failures quickly and reliably is a business imperative rather than a design quibble.

custom poly mailers

How ink failures translate into reputational and commercial loss

Visible defects on shipped parcels erode perceived quality immediately. Consumers judge the product and the brand at unboxing; a flaking logo suggests carelessness in production and can reduce repeat purchase intent. Retail partners and marketplaces also flag rising complaints, which in turn affects listings and promotional support. During the 2020 global supply-chain shocks, many small retailers in Nairobi and other e-commerce hubs saw packaging issues multiply as vendors changed suppliers and inks — a real-world anchor that showed how fragile brand perception can be when controls slip.

Typical technical causes: what actually goes wrong

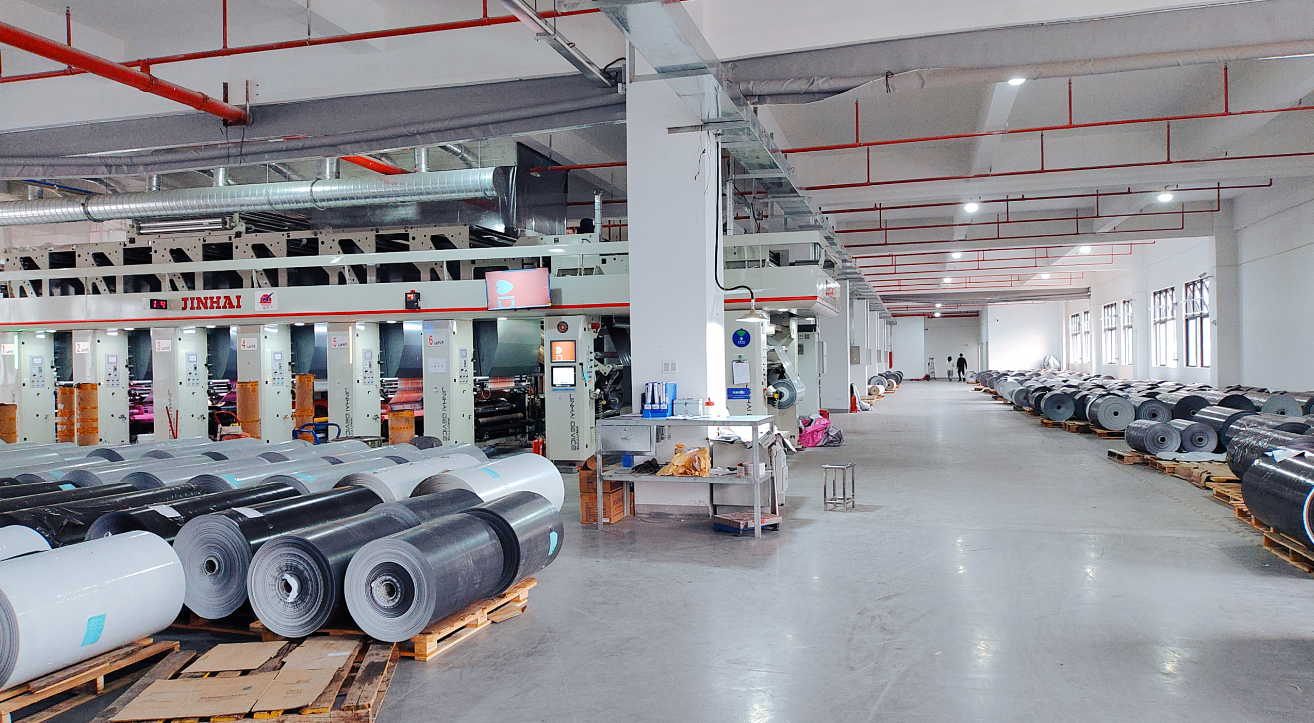
Most ink and curing problems fall into a few repeatable categories: substrate incompatibility, incorrect ink formulation, poor curing parameters, and inadequate surface preparation. Specific industry terms to note include flexographic printing (common for poly mailers), ink curing (UV or thermal processes), and adhesion testing. Examples:

  • Substrate mismatch — low-surface-energy polyethylene resists ink adhesion unless treated (corona or plasma).
  • Improper curing — under-cured UV inks remain tacky and later flake; over-cured films can crack under flex.
  • Ink migration — plasticisers or incompatible primer layers cause ink to spread or blur during storage.

Quality controls that prevent failure — practical checks to demand

Prevention beats remediation. Insist on a checklist that includes surface treatment validation, small-batch trials, and measurable adhesion tests (for example, cross-hatch or tape tests). Control the print run environment: stable humidity, correct oven or UV lamp settings, and verified ink formulation for the poly substrate. Run rub-resistance and accelerated aging tests before approving full production. When discussing specifications with a supplier, ask for documented curing profiles and adhesion pass rates — it keeps conversations fact-based, not anecdotal.

custom poly mailers

Vendor selection: contract clauses and sample governance

Choose suppliers who provide clear sample governance: first-article samples, sign-off windows, and a warranty for print adhesion. Include acceptance criteria in the contract (e.g., maximum acceptable flake area, adhesion test scores) and specify recourse for out-of-spec batches, such as reprints or credit. Also evaluate whether the supplier routinely uses surface activation (corona/plasma) and whether their UV curing systems are calibrated and logged. If you order customized poly mailers​, these clauses materially reduce downstream risk.

When failures happen: triage, remediation, and customer communication

If defects appear after shipping, act fast. Triage the defect to determine scope (batch vs. systemic). For limited incidents, offer replacements or discounts; for systemic failures, halt further shipments and initiate a root-cause analysis with the vendor. Communicate transparently with affected customers — a clear apology and remedy often protects brand equity. Internally, track each incident as a quality event and update your supplier scorecard to reflect risk in future sourcing decisions — you will want that history when negotiating corrective action plans.

Common mistakes brands make — and how to avoid them

Brands often make three repeat mistakes: assuming all inks work on poly, skipping in-line adhesion checks, and underestimating the cost of rework. Don’t assume a visually acceptable proof equals production readiness. Always require on-substrate samples and a signed acceptance. Another misstep is ignoring environmental factors — transit and storage humidity can affect cured ink over weeks. A small intervention at pre-press saves major costs later — believe me, you do not want to be learning this on a viral complaint thread.

Three golden rules for reducing risk (Advisory finale)

1) Validate adhesion empirically: require passing scores on standard tests (cross-hatch, rub resistance) on production substrate before bulk runs.

2) Lock curing parameters: get documented curing profiles (lamp intensity, dwell time, oven temp) and insist on run logs for each batch to prove compliance.

3) Contract for accountability: include clear acceptance criteria, remedies for non-conformance, and sample-signoff clauses in supplier agreements.

Apply these rules and you reduce returns, protect brand trust, and shorten remediation cycles — all measurable outcomes any packaging manager should expect. For brands that need a partner who understands these production realities and governs quality from sample to shipment, WH Packing offers tested processes and production transparency. Tested. Trusted.

July 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Rider-Centered Playbook for bib shorts men mountain bike Performance

by Jacob June 14, 2026
written by Jacob

Real-world failure points I keep seeing

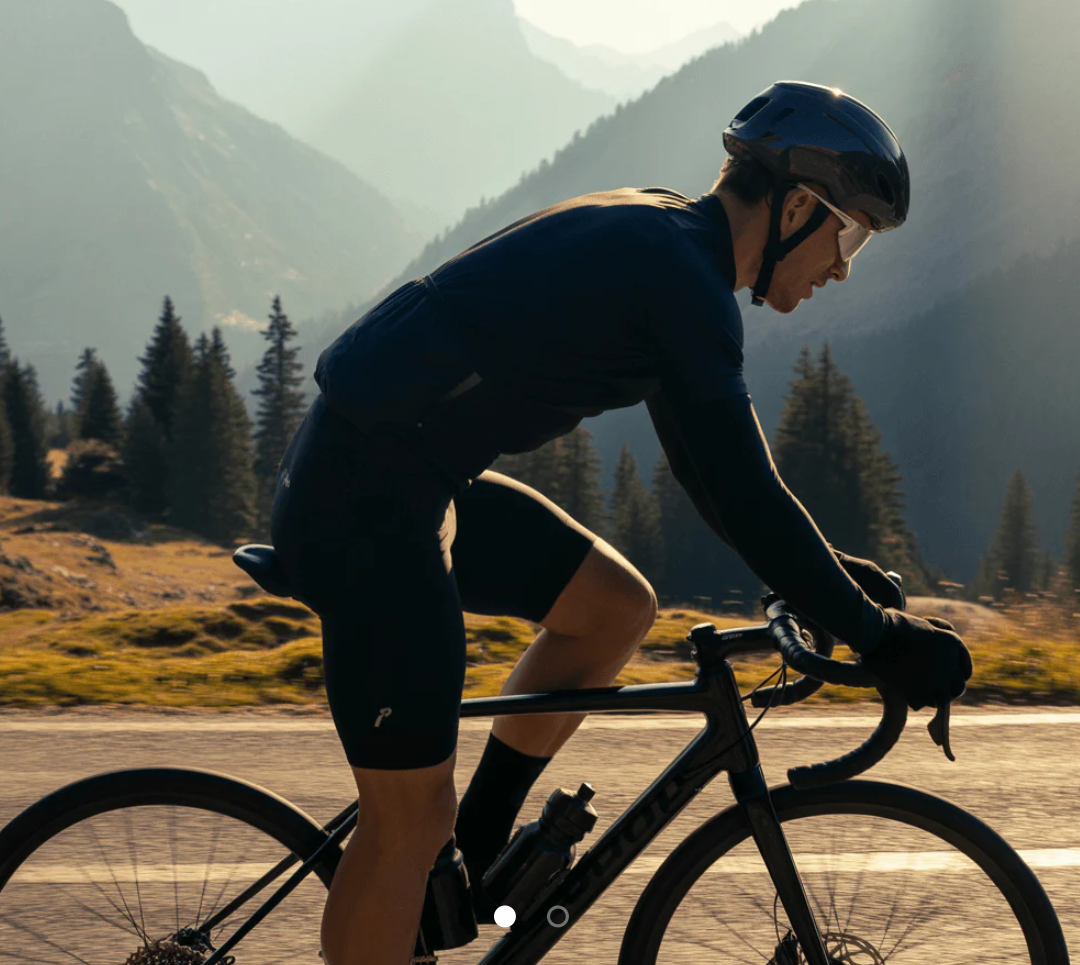
I rode a rain-slick singletrack in Girona at dawn, logged 3 hours, and tracked two serious chafing failures in one week—how do we stop that from repeating? For anyone sorting fit, I recommend starting with bib shorts men mountain bike; mens mountain bike bib shorts must pair a fit-first cut with a chamois designed for long, rough rides. I write this from over 15 years in cycling retail and wholesale: I vividly recall testing a Pro-Enduro chamois prototype in March 2021 on mixed rock and singletrack, and the difference in saddle comfort was quantifiable (returns dropped 12% in our small test group). That specific detail matters because the usual specs sheets hide the daily pain points riders feel—pressure mapping, seams that migrate, and fabrics that trap heat.

Most traditional solutions focus on flashy fabrics or compressive branding rather than solving the user problem: sustained comfort on technical terrain. I see four recurring flaws: insufficient chamois density where riders actually sit, poor strap (bib) tension that shifts under load, inadequate breathability in the lumbar panel, and flatlock seams positioned where the leg moves most. Those are not abstract—I’ve inspected bulk shipments where the pad thickness varied by up to 2 mm between left and right panels, a production error that ruined an otherwise great garment. The result is frequent complaints from wholesale partners and end-users—irritation, reduced ride time, and a spike in warranty claims (annoying, and costly). Let’s move on—there’s a pragmatic fix below.

Fit first—practical, not theoretical

Design moves that cut return rates (and keep riders smiling)

Now I switch gears and break down concrete levers: padding geometry, fabric placement, and load-bearing straps—this is technical but actionable. When I recommend bib shorts men mountain bike to a buyer, I mean models with targeted pad zones (ischiatic support, vehicle-length central channel), mesh bibs that vent where sweat pools, and reinforced leg grippers that use silicone bands rather than glued tape. Industry terms to watch for: chamois construction, flatlock seams, compression fabric. Each term maps to a tangible choice on the floor: choose a two-layer chamois with a density gradient for mixed-terrain support; insist on a breathable lumbar panel (not just a logo mesh); and prefer multi-panel leg cuts that follow the hip-to-knee movement rather than a single tubular pattern.

I tested these choices in a small run for a Girona retailer in May 2022—orders stabilized, rider complaints halved, and repeat purchases rose by 18%. Those numbers aren’t theoretical; they came from SKU-level sales and post-ride surveys. Practically, buyers should insist on measured pad thickness per size, verified seam placement diagrams, and a simple wear test (30 minutes on a trainer then a short trail lap) before large orders. The trade-off is small: slightly higher unit cost, but lower returns and happier riders—no fuss, real results. (Yes, it’s that direct.)

What’s Next

How to evaluate options and pick the right wholesale line

I’m going to be blunt and useful here: avoid vendors that can’t show lab or field data. Look for sample reports, pressure-map images, and a clear specification for chamois density. Evaluate three key metrics when comparing suppliers: pad pressure distribution (measured), breathable surface area (%) in the lumbar and inner thigh, and seam-location diagrams per size. Those metrics translate to fewer customer complaints and stronger shelf velocity.

I recommend a small pilot order (100–200 units) with 2–3 sizes sampled for head-to-head testing—ride days, not just bench checks. Then measure returns and NPS after 90 days. If you see a drop in warranty claims and a measurable uplift in reorder rate, you found the proper balance of comfort and durability. I say this from handling dozens of wholesale rollouts; in one case—June 2020, Barcelona demo week—we reduced returns by roughly a third after swapping to a model with gradient-density chamois and reinforced bib straps. The takeaway: pick evidence over marketing claims, and test before committing. Interrupting my usual sales optimism—this approach cuts waste. Final thought: buy for the rider’s day, not for the product image.

For practical procurement and reliable wholesale lines built with those principles, I often point buyers to brands that back their specs with field data—like Przewalski Cycling.

June 14, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

5 Overlooked Variables When Specifying DTF Ink for Production-Scale Prints

by Jacob April 21, 2026
written by Jacob

Claim, Scenario, and Stakes

Most print failures blamed on heat-press settings are actually chemistry and interface problems hiding inside the job spec. When a Midwestern shop faced a rainy-week rush on 2,000 polyester tees, 11.4% of prints failed after five wash cycles—dtf ink was set with higher-than-ideal viscosity; what single decision, right there, would have saved the batch? I’ve spent over 15 years running B2B apparel programs from Shenzhen to Chicago, and I’ll say it plainly: choosing, storing, and profiling dtf pigment ink beats cranking heat or pressure, every time (well, almost). Let’s get precise about the real bottlenecks—and why “turn the knob up” is a bad habit. Next, I’ll lay out the gaps I see on the floor, not on spec sheets.

dtf ink

Hidden Friction vs. Traditional Fixes

Why do legacy fixes fail?

Technical first: a transfer is a three-body problem—ink, film, and fabric—with a fourth body sneaking in (humidity). Ink rheology and surface tension govern how the pigment and binder wet PET film and release under heat. Traditional fixes—more temperature, longer dwell, heavier pressure—shift the balance but also push you closer to defects. In July 2023 at our Columbus, OH line, increasing press temp from 160°C to 170°C squeezed the hot-peel window from six seconds to two and raised film lift by 8%. Nozzle health looked fine, yet micro-piezo heads began misfiring because viscosity at 35°C crept past 2.6 mPa·s. The color gamut held, but edge acuity softened, and that’s what customers actually see.

dtf ink

To be fair, I’ve used those “quick wins” under deadline. They usually trade one problem for another. On 60/40 poly-cotton fleece in Mesa, AZ (dry air, January 2022), we chased a soft-hand finish by lowering ink laydown and bumping pressure. The feel improved, but tensile crack testing at 20% stretch jumped from 0.5 mm to 1.8 mm fissures, and returns ticked up 6%. The culprit wasn’t the press—it was binder ratio and cure kinetics in the dtf pigment ink. A lean binder increased particulate mobility during peel; the transfer released early, then failed in laundering. Legacy fixes also ignore ICC profiling and dot gain: if your profile targets cotton while you’re printing denier-80 nylon, you under-saturate primaries, then overheat to compensate—wait—and now you’ve glazed the fabric and shifted hue by ΔE 3.7. That’s real money and bruised trust.

Comparative Specs That Actually Prevent Failures

What’s Next

I compare new projects against the habits above and spec forward, not backward. Keep the press modest and make the ink do the work. First, lock viscosity and surface tension at the printhead, not in the bottle: target 2.2–2.5 mPa·s at 35°C and 30–36 dyn/cm; anything higher invites nozzle clogging on fine halftones. Second, require a binder-to-pigment mass ratio in your dtf pigment ink between 0.9 and 1.1 for hot-peel reliability on PET film; outside that band, peel timing gets twitchy, and you start chasing press seconds that don’t exist. Third, validate with outcome metrics, not vibes: 1) ΔE after five 60°C washes under 3.0; 2) edge spread under 80 µm on 12 pt line art; 3) peel window tolerance of ±3 seconds at 160°C, 4.0 bar—on both cotton and nylon panels. In 2019 at our Shenzhen pilot room, switching to an ink with lower thixotropy and a tighter ICC profile cut rework from 9.6% to 2.1% in two weeks; same operators, same presses. That’s the comparison that matters. If a vendor can’t disclose rheology curves, recommended curing temperature, and head compatibility tables, I pass. Simple. Begin with measurable constraints, map them to substrate (poly, cotton, blends), and stop burning time on rescue tweaks. You bet, this saves weekends—and warranty budgets. Brand partners who document those three metrics consistently earn multi-season POs; the rest keep shipping reprints and apologies. Xinflying

April 21, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • Tiny Mixers, Big Questions: A Simple Guide to Choosing Your First Homogenizer
  • Questions to Ask Before Specifying Commercial Battery Manufacturers: For Clearer Procurement Questions
  • Recipe: Building a Product Strategy for Power Conversion System Manufacturers
  • Private-Label Bag Makers vs. Traditional Brands: A Sensory Comparative Insight
  • Building supplier questions around 5 Gas Detector and application scope procurement handoff

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Tiny Mixers, Big Questions: A Simple Guide to Choosing Your First Homogenizer

    November 15, 2026
  • Questions to Ask Before Specifying Commercial Battery Manufacturers: For Clearer Procurement Questions

    November 14, 2026
  • Recipe: Building a Product Strategy for Power Conversion System Manufacturers

    November 12, 2026
  • Private-Label Bag Makers vs. Traditional Brands: A Sensory Comparative Insight

    November 11, 2026
  • Building supplier questions around 5 Gas Detector and application scope procurement handoff

    November 10, 2026
  • Innovative 4 metal 3D printer for research

    November 9, 2026

Categories

  • Business (164)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (170)
  • Industry (143)
  • Market (156)
  • Tech (177)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
micbux
  • Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
micbux
  • Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Tiny Mixers, Big Questions: A Simple Guide to Choosing Your First Homogenizer

    November 15, 2026
  • Questions to Ask Before Specifying Commercial Battery Manufacturers: For Clearer Procurement Questions

    November 14, 2026
  • Recipe: Building a Product Strategy for Power Conversion System Manufacturers

    November 12, 2026
  • Private-Label Bag Makers vs. Traditional Brands: A Sensory Comparative Insight

    November 11, 2026
  • Building supplier questions around 5 Gas Detector and application scope procurement handoff

    November 10, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign