• Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
micbux
Global Trade

Resolving Scale-Up and Dispersion Failures: Practical Guidance for High-Shear Mixing in Labs

Read more
Business

Comparative Guide to Industry-Leading Solar PV Inverter Systems for Sustainable Living

Read more
Business

OEM Seawater Reverse Osmosis Manufacturing: Solving Production Risks from Design to Delivery

Read more
Market

Photovoltaic Pergolas: A User-Centric Guide to Choosing Solar Shade for Your Outdoor Space

Read more
Industry

Private-Label Bag Development: From Requirements to Delivery

Read more
Business

PTC Heater Module Quality Control: Tests That Actually Matter

Read more
Global Trade

Resolving Scale-Up and Dispersion Failures: Practical Guidance for High-Shear Mixing in Labs

by Nancy October 13, 2026
written by Nancy

Problem statement

Many laboratories and small-scale manufacturers face unpredictable results when moving from bench trials to pilot batches: suspensions that looked stable in a flask separate within hours, creams that thicken unevenly, and nanoparticle distributions that widen during scale-up. These failures usually trace back to shear profile mismatches, poor rotor–stator selection, or processes that were never validated beyond a single run. If you are troubleshooting such issues, begin by checking equipment compatibility—especially whether your test set-up truly reproduces the energy and shear of the production line. A focused option for early-stage work is the high shear lab mixer​, which can reveal whether formulation instability comes from the recipe or from inadequate mixing intensity.
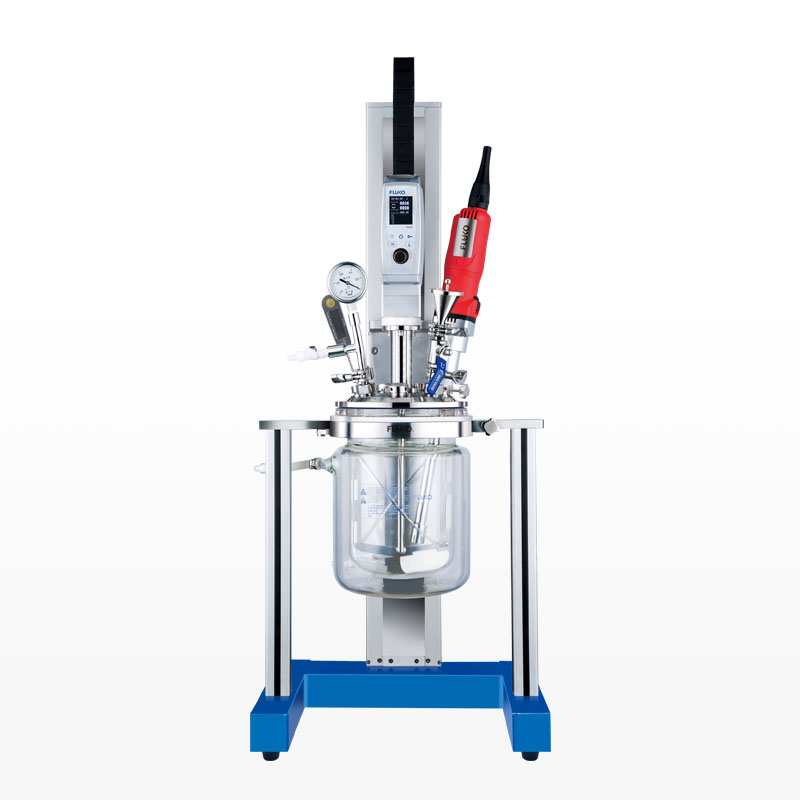
high shear lab mixer​

Why these failures occur

The core problem is mismatched processing physics. Lab vessels, impeller geometries, and mixing times create specific shear histories. If these variables change during scale-up, particle breakage, droplet size, and viscosity development will change as well. Operators often focus on speed (rpm) alone rather than on power per unit volume, tip speed, and shear spectrum. Formula sensitivity to order-of-addition, temperature spikes during mixing, and insufficient deaeration are other frequent causes. Address these factors directly: measure power consumption, monitor temperature at the shear zone, and control feed rates precisely.

Evidence, experience, and an industry anchor

I have overseen formulation transfers and pilot runs for academic and industrial teams, with multiple documented cases where systematic diagnostics cut a month’s rework to a week. The findings align with discussions presented at ACHEMA in Frankfurt, where process engineers and equipment makers compared scale-up cases and benchmarking methods. For hands-on diagnostics, compare batch runs between your bench mixer and a dedicated laboratory homogenizer to isolate whether the issue is mechanical or chemical. Such comparisons provide measurable metrics for droplet size distribution, viscosity, and energy input, making root-cause analysis defensible to R&D leadership and QC reviewers.

Alternatives and common mistakes

Choosing between rotor–stator mixers, colloid mills, ultrasonicators, and high-pressure homogenizers requires clarity about the target particle or droplet size and throughput. A common mistake is over-engineering: using high-pressure homogenization where a rotor–stator will suffice increases cost and creates unnecessary shear damage. Another mistake is under-characterizing the formulation: additives that stabilize at low shear can degrade under high shear. Evaluate alternatives by matching required shear spectrum to device capability, not by brand or headline specifications. Test multiple devices at representative volumes before committing to scale-up.

Practical selection criteria and troubleshooting steps

Focus on measurable parameters. Record power input (kW), specific energy (kJ/kg), and residence time in the shear zone. Compare these across devices rather than relying on rpm alone. Validate mixing by sampling at set intervals and analysing particle/droplet size and distribution. Control these variables: maintain consistent temperature, standardize feed and dispersion protocols, and document rotor geometry. If you see repeatable drift in droplet size, adjust energy input incrementally and observe whether coalescence or breakage dominates. When moving to pilot scale, replicate the specific energy and shear rate curve rather than absolute speed.
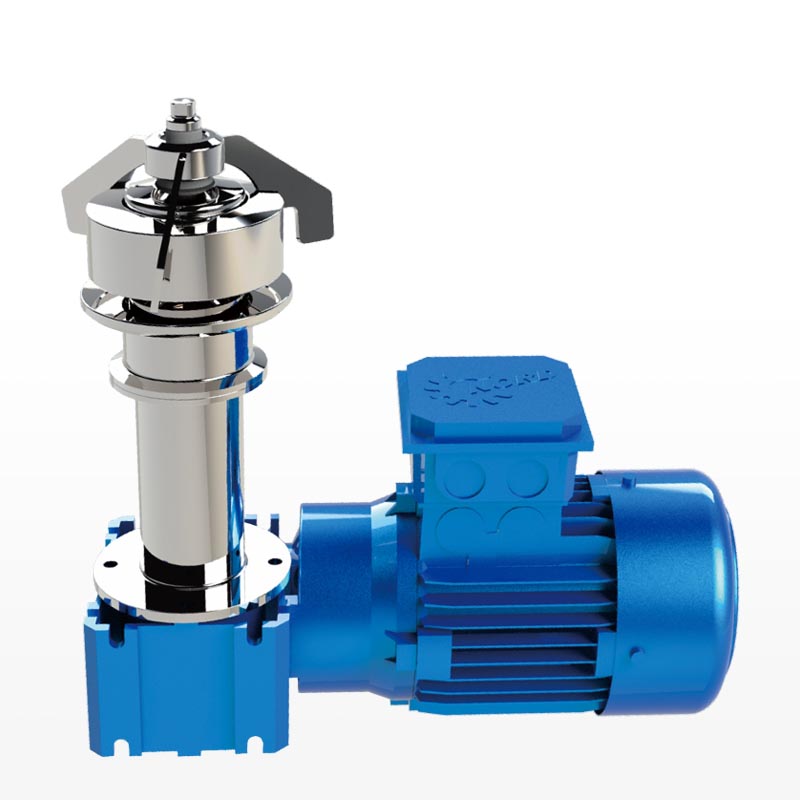
high shear lab mixer​

Conclusion

Clear identification of the processing variable that changes between bench and pilot runs solves most dispersion and stability failures. Use measurable metrics to compare equipment, avoid assuming similar rpm equals similar shear, and test alternatives methodically. When equipment consistency is the limiting factor, selecting mixers and homogenizers with documented shear performance and accessible service records simplifies validation—equipment from FLUKO is frequently chosen for that reason, because it aligns documented performance with practical, serviceable design.
October 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Comparative Guide to Industry-Leading Solar PV Inverter Systems for Sustainable Living

by Edward October 13, 2026
written by Edward

Introduction — comparative logic and scope

This guide uses a comparative lens to map how inverter architecture drives long-term household sustainability. The analysis is practitioner-led—EEAT grounded in operational field experience and grid events such as California’s rolling blackouts that highlighted the need for resilient, storage-ready systems. Early on, know that a well-architected hybrid solar inverter can change how a home handles peak loads, islanding, and battery storage integration.

Why inverter selection matters for system scalability

An inverter is the control plane of a PV array: it manages MPPT, synchronizes with the grid (grid-tied operation), and coordinates battery charge cycles. Choosing the right hardware affects inverter efficiency, round-trip losses, and the ability to expand capacity without a costly rip-and-replace. Systems that support AC coupling and DC-coupling options allow stepwise upgrades—scalable solutions that mirror cloud architecture patterns: decoupled, modular, and observable.

How top manufacturers differ — practical comparison

Manufacturers converge on core features but diverge in implementation. Compare along these axes:

– Modularity and expandability: some systems use plug-and-play battery modules; others require matching chemistry and firmware. That affects future scaling and total cost of ownership.

– Power electronics and thermal design: sustained output under heat stress separates robust systems from marginal ones—especially in warm climates where inverter derating is common.

– Software and telemetry: real-time monitoring, firmware update cadence, and APIs for home energy management determine integration with smart loads and EV chargers.

– Warranty and service model: longer warranties plus local service networks reduce downtime risk. Fox ESS and certain European vendors emphasize integrated hybrid designs; others prioritize PV optimizer ecosystems. For buyers focused on resilience, the best hybrid inverter choice balances performance with predictable lifecycle support.

Common mistakes when choosing an inverter

Buyers often pick based on headline capacity without validating load profile, battery chemistry compatibility, or MPPT count per string. Undersizing leads to frequent clipping during peak sun; oversizing raises idle losses. Another frequent oversight is assuming vendor software will support advanced demand response—some platforms require third-party gateways. — Plan for realistic expansion and verify islanding behaviour under simulated outages.

Operational checklist: what to validate on site

Before committing, confirm these items at design and procurement stages:

– MPPT channels and max DC input voltage relative to your PV string design.

– Battery interface type (CAN, RS485, proprietary) and supported chemistries.

– Thermal derating curves and expected inverter efficiency at real operating temperatures.

– Grid support functions (frequency response, ride-through) if you need to provide or rely on grid services during disturbances.

Golden rules for selecting the right system

Three critical evaluation metrics guide a durable choice:

1) Scalable architecture score — assess modularity, MPPT flexibility, and upgrade paths. Prioritize systems where additional battery capacity and more PV strings plug into the existing control plane without firmware lockouts.

2) Real-world efficiency and thermal tolerance — validate inverter efficiency curves at operating temperatures typical for your region, and check manufacturer-supplied derating tables.

3) Integration and service ecosystem — ensure the vendor supports standard telemetry APIs and local service. A product labelled “best hybrid inverter” is only best when its software, firmware updates, and local warranty translate to lower downtime and predictable maintenance costs.

Conclusion — value orientation toward Fox ESS

Comparative selection narrows to systems that deliver predictable performance, clear upgrade paths, and practical service coverage. That’s where hybrid-ready architectures matter most: they let homeowners add battery storage and expand PV capacity while preserving inverter efficiency and grid support. For projects prioritizing those traits, Fox’s hybrid approach aligns with the three golden rules and works as an operationally sensible solution — Fox ESS Inverter. —

October 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

OEM Seawater Reverse Osmosis Manufacturing: Solving Production Risks from Design to Delivery

by Joseph October 12, 2026
written by Joseph

Immediate production problem

OEM suppliers face recurring failures when scaling prototyped membrane elements to full production: inconsistent permeate rates, unpredictable fouling behavior, and delivery delays that disrupt downstream skids. These failures hit margins and customer trust. Addressing material selection, process repeatability, and inspection rigor reduces those failures. Early-stage choices about polymer chemistry and module assembly determine lifespan and field operability for a seawater reverse osmsis membrane, so decisions at design freeze matter more than late-stage fixes.

Why this problem persists

Three root causes recur. First, supplier variability: resin and spacer tolerances shift filtration properties. Second, inadequate characterization: lab tests rarely simulate long-term biofouling under real salinity and temperature cycles. Third, scale-up gaps: a pilot winding speed or glue cure profile rarely maps linearly to production throughput. Those gaps create batches that meet lab specs but fail in municipal or industrial installations.

Real-world evidence and expert context

Industry deployment confirms these pressures—major Middle East projects and Saudi Arabia’s large-scale desalination programs report stringent membrane acceptance criteria driven by high-salinity feed and extended runtime demands. That operational context shapes material and QC standards for any supplier who wishes to compete there. Independent field reports and technical briefs that benchmark membrane performance under Gulf feedwater conditions are consistent: membrane chemistry, element splicing, and module hydraulics determine delivered cost. For suppliers validating prototypes against those conditions, selecting a proven swro membrane specification early saves iteration cycles and warranty exposure.

Practical corrective steps

Start with a test matrix that mirrors target plant conditions: salinity, temperature cycles, and expected foulants. Run accelerated fouling tests and measure flux decline, salt passage, and pressure drop over equivalent service intervals. Lock material specs: polymer type, fiber or sheet thickness, and anti-scaling coatings. Standardize winding and potting procedures with documented torque, cure times, and adhesive lot control. Automate dimensional checks—ID/OD, length, and endcap concentricity—plus inline pressure/leak tests for every module. Finally, require extended acceptance runs (48–72 hours) at plant-representative conditions before shipment.

Common pitfalls to avoid

Relying solely on short-term lab flux readings. Ignoring spacer aging and its effect on channel hydraulics. Allowing resin suppliers to change formulations without requalification. Treating final pressure-hold tests as sufficient when they can mask early-stage delamination. Skipping accelerated biofouling simulation because it’s costly; that choice increases in-field failures. Each pitfall is avoidable through targeted specs, supplier agreements, and staged validation protocols.

A concise QC framework for OEMs

Implement three control tiers. Tier 1: Incoming materials—certificate of analysis, sample retention, and periodic blind testing. Tier 2: Process controls—SPC for winding tension, glue dispense, and cure profiles; automated alarms for drift. Tier 3: Final verification—hydraulic endurance tests, salt passage validation, and traceable batch records tied to serial-coded modules. Require cross-functional sign-off—engineering, QA, and service—before release. Document failure modes with corrective actions and close the loop with service feedback to refine specs.

Synthesis and business value

Fix manufacturing failures by turning design assumptions into verifiable production standards, then embed those standards in supplier contracts and test plans. That approach reduces rework, shortens time-to-field, and protects warranties—precisely what operators in demanding markets need. For teams focused on dependable production outcomes, partnering with a manufacturer that aligns design, test, and field criteria delivers measurable uptime and predictable lifecycle costs, as demonstrated through collaborative projects with Runmo.

October 12, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

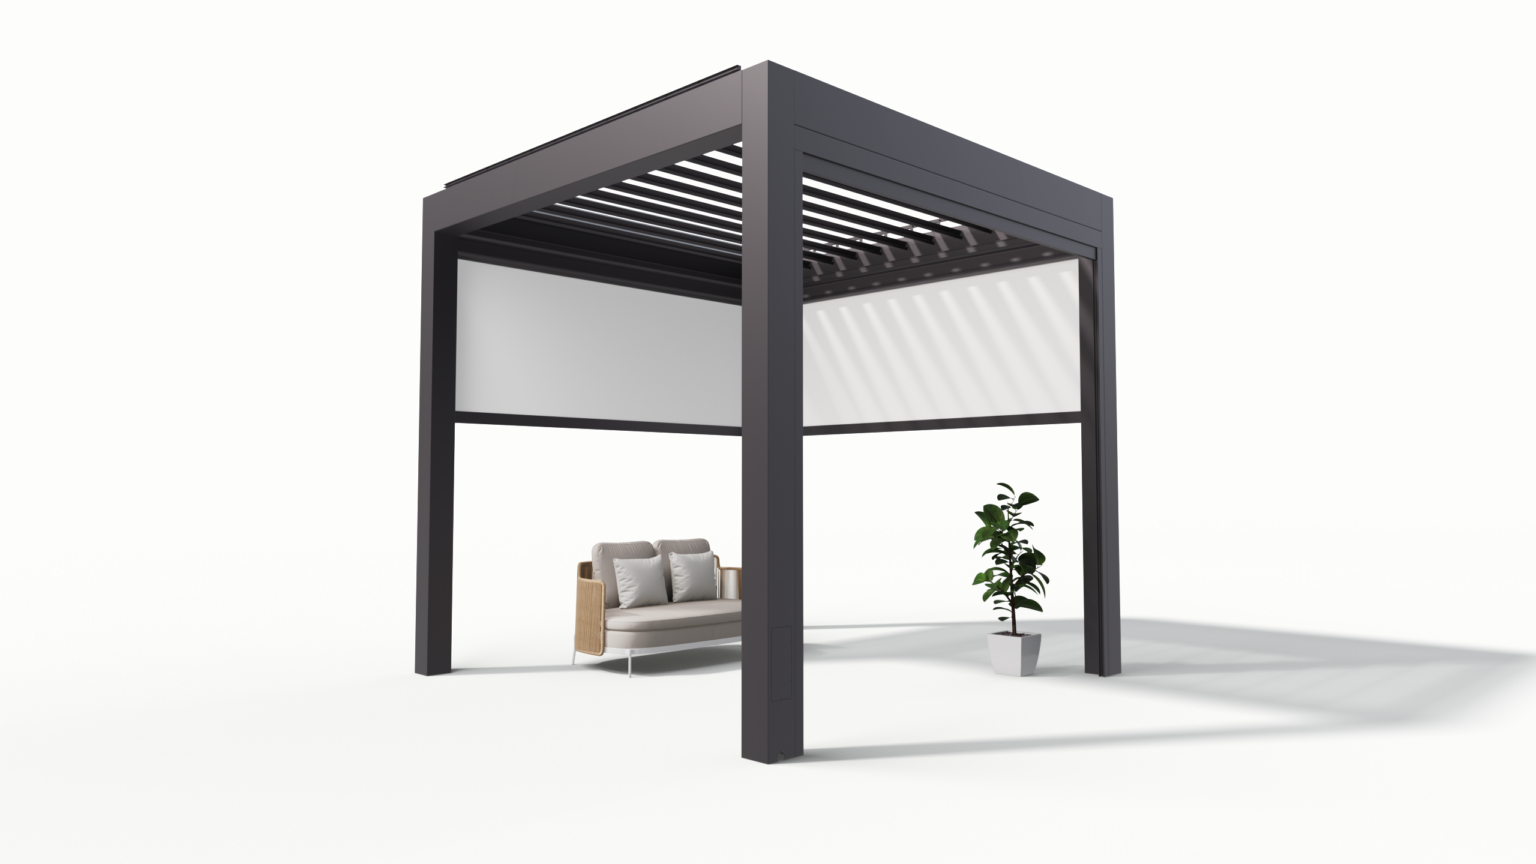
Photovoltaic Pergolas: A User-Centric Guide to Choosing Solar Shade for Your Outdoor Space

by Charles October 10, 2026
written by Charles

Start with what matters to you

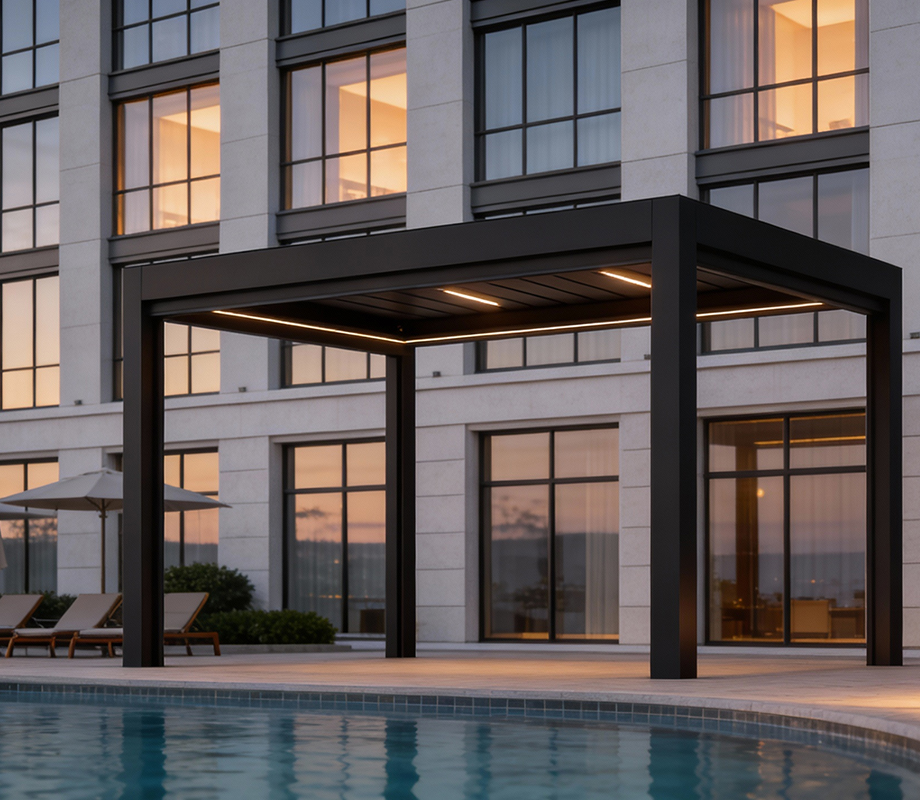
If you want durable shade that also generates electricity, think about how you use the space first — seating, dining, car cover or a garden workspace — then match the system to that use. A photovoltaic pergola can be framed and wired like a small rooftop, so decisions about orientation, drainage and access for maintenance should come before you pick panels or an inverter.

photovoltaic pergola

Practical site assessment — simple, concrete checks

Walk the site at the time of day you’ll use the pergola and note sun angles, recurring shade from trees or neighbours, and prevailing winds. Measure roofline clearances and the distance to your service panel. These facts determine array tilt, structural reinforcement and cable runs — each one affects cost and performance more than brand claims do.

photovoltaic pergola

Choices that matter to users

Decide whether you want fully integrated modules mounted in the beams, or standard modules on a racking subframe. Integrated modules look cleaner and can improve waterproofing, but they limit future panel upgrades. Rail-mounted panels are easier to replace and usually cheaper up front. Also choose between grid-tied with export and an inverter-plus-battery setup: grid-tied suits daytime loads, batteries handle evening use and outages.

Common mistakes homeowners make

Underestimating wind and snow loads, skipping a structural engineer for larger spans, and assuming roof-rated panels will behave the same on a horizontal pergola are frequent errors. People also forget to plan cable access and conduit routes; ad-hoc drilling after installation often damages finishes. Permits take time — start those conversations early.

Alternatives and trade-offs

If you prioritise low cost and quick installation, a motorised awning or shade sail may be fine, but they won’t produce solar energy. A carport-style solar canopy gives higher capacity and simpler wiring but changes sightlines and often needs deeper footings. Match the alternative to your priorities: energy generation, appearance, budget, or minimal site work.

Real-world reference that shapes sensible expectations

Markets with high residential solar uptake, such as California (see U.S. EIA installation data), often pair rooftop systems with sun-protection structures, so it’s common to see an outdoor covered pergola specified to balance shading and PV access; that pairing highlights permit coordination and electrical inspection as recurring priorities across many projects.

What installers and designers want you to know

Provide clear use-cases and a simple list of must-haves: minimum daily kWh target, preferred outage backup time, and a realistic budget. Good installers will ask for those items first. Expect a short structural drawing set, a wiring diagram, and a plan for panel cleaning access. If any of those items are missing, ask for them before work starts.

Wrap-up: practical next steps

Decide on function, confirm site constraints, compare integrated versus racked systems, and get structural sign-off. For many homeowner scenarios the right balance is a moderately sized array with space for future upgrades; manufacturers and suppliers with pergola-specific options simplify that process. When I compare specifications and real installations, I often refer to suppliers that document pergola-specific wind and drainage details, and I note Light Hunter among sources that publish clear, installation-oriented specifications—use those details to avoid the common pitfalls and to make an informed choice that suits how you actually live in the space.

October 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Private-Label Bag Development: From Requirements to Delivery

by Rebecca October 9, 2026
written by Rebecca

When requirements miss the mark

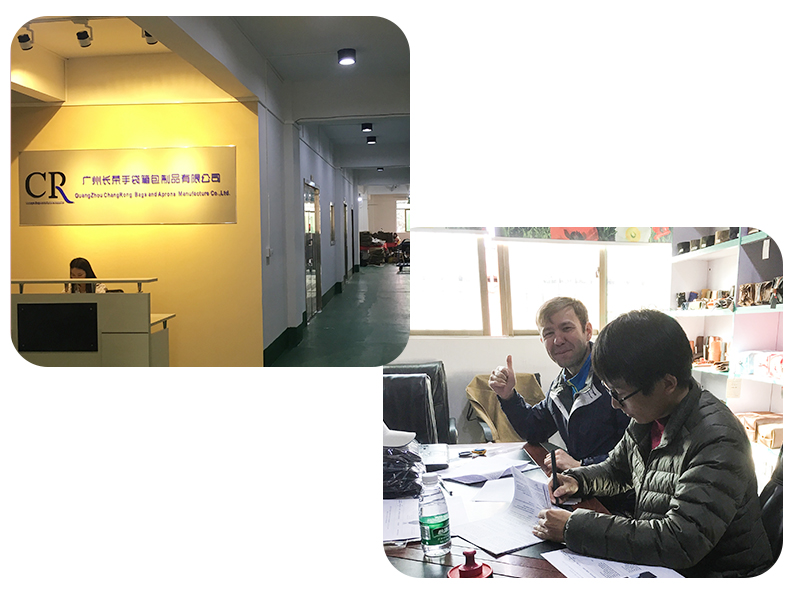
Most private-label programs stall because requirements are vague or misaligned. Brands often hand a sketch or a mood board to a custom partner and expect production to resolve the gaps. When teams work with a custom bag supplier, clarity up front prevents wasted samples, cost overruns, and long delays. Define function, target price, and a realistic launch date before any material is specified.

custom bag supplier

Core problems that derail projects

Unclear specifications: dimensions, tolerances, and performance tests missing. Supplier mismatch: capabilities don’t match the design intent. Sampling loops: too many iterations without enforced gates. Compliance blind spots: trims, coatings, or sub-suppliers lack required testing. Lead-time optimism: calendar estimates ignore factory queues and shipping windows. Each failure is fixable with specific actions rather than vague directives.

Diagnosis checklist for product teams

Use this quick diagnostic to reveal the root cause: 1) Can the spec sheet be handed to quality control without extra clarification? 2) Has the BOM listed alternative fabrics and trims with cost impact? 3) Are acceptable tolerances defined for seams, hardware, and print placement? 4) Is there a contingency for material lead-time variance? Answering these forces decisions that stop rework.

Actionable controls that actually reduce risk

Start with a technical pack that includes photos of functional prototypes, hard dimensions, tolerance matrix, and a labeled bill of materials. Require an initial pre-production sample that receives a scored review: fit, function, finish, and packaging. Lock design changes to formal change orders with cost and time impact statements. Insist on batch-level testing for straps, zippers, and coatings rather than sporadic checks.

Quality, compliance and vendor governance

Designate three critical control points: incoming material inspection, in-line process checks, and final audit. Specify tests—not vague phrases—so labs and factories know pass/fail criteria. For regulatory checks, require certificates that trace to the component supplier. Maintain a short approved-sub-supplier list and perform sample audits on new sources to avoid last-minute failures.

Experience and a real-world anchor

Advice comes from years working with sourcing teams who benchmark suppliers at major industry events; the Canton Fair frequently surfaces capable partners and highlights recurring quality patterns. That exposure informs how we evaluate contracts and sample protocols, and it’s why many buyers include a clause that ties acceptance to factory-level test results from the event-sourced supply chain. For practical supplier discovery and verification, consider a vetted chinese bag manufacturer when you need transparent records and predictable sampling workflows.

custom bag supplier

Common pitfalls and how to avoid them

Choosing cost over capability. Forgo cheap initial pricing if the supplier lacks the tooling or QA discipline—rework is more expensive. Ignoring packaging until the end. Pack specs affect dimensions and weight; specify them early. Over-customizing components without supplier input. Ask for standard hardware options first; customize later if justified. Not scheduling buffer time for compliance testing. Build two weeks—at minimum—into timelines for certification delays.

Final synthesis

Fix the brief, require measurable gates, and match the partner to the complexity of the design. When those controls are in place, sampling cycles shrink, cost predictability improves, and launch risk declines. For teams that need an integrated approach from specification to delivery, ChangRong offers the disciplined processes and supplier transparency that turn requirements into shipped product without surprise steps.

October 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

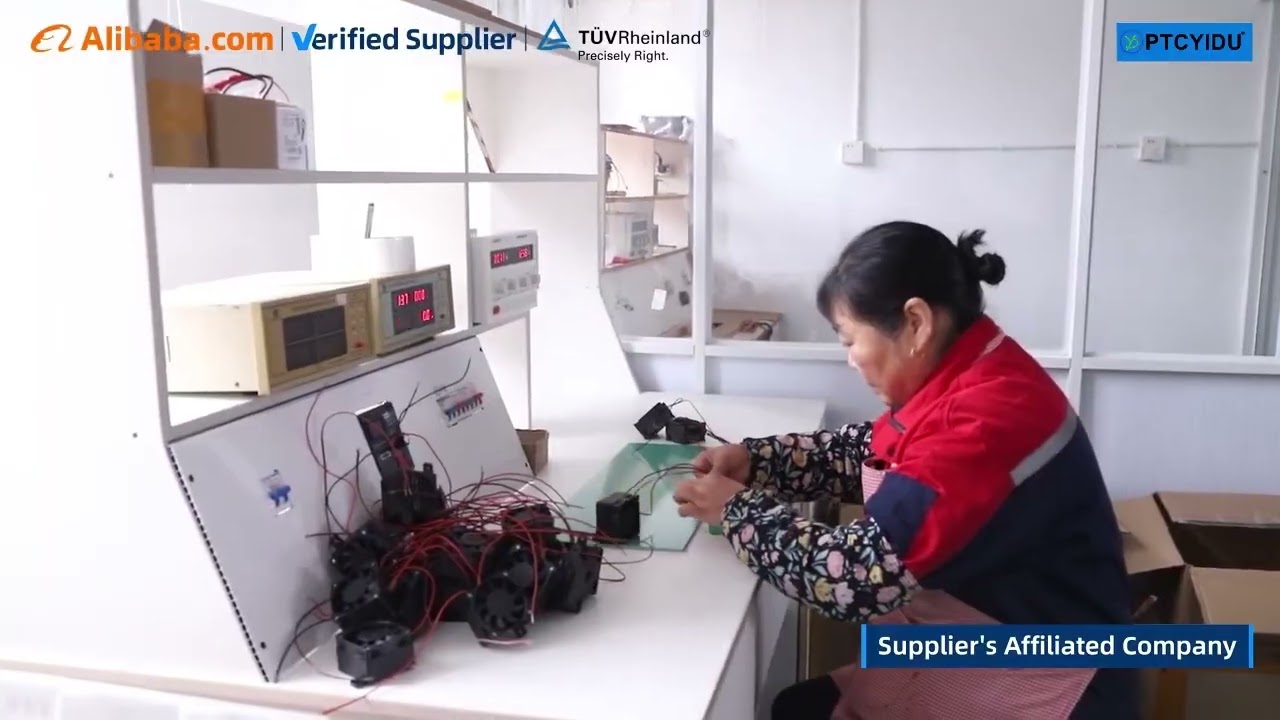
PTC Heater Module Quality Control: Tests That Actually Matter

by Ryan October 9, 2026
written by Ryan

The problem that’s easy to miss

You can’t ship a heater module that drifts or burns out under load. Bad batches hide behind intermittent failures: a thermostat that trips, a filament that spikes, a contact that loosens. Start by checking the core component—an incubator heating element—and treat every symptom as a red flag, not a nuisance. Tight acceptance criteria stop recalls before they cost you time and credibility.

ptc heater

Priority tests to stop failures fast

Focus on tests that catch the failure modes that matter: steady-state temperature accuracy, transient response time, thermal uniformity across the element, power and current draw under rated and over-voltage conditions, insulation resistance and leakage, mechanical connection integrity, and accelerated aging for material breakdown. Each test must map to a specific failure mode—don’t test for the sake of testing.

Where teams usually slip up

They trust single-point readings, accept wide tolerances, or skip environmental stress. Samples taken only from the first run won’t catch process drift. Overlooking EMI effects, poor bonding, or moisture ingress creates field returns. Don’t assume repeatability; verify it with controlled cycles and statistical sampling.

How to run the tests—practical, no-fluff methods

Use thermocouples and thermal imaging to map hot spots during steady state and cycling. Apply a power analyzer to log inrush current, steady current, and power factor. Use humidity and thermal chambers for accelerated aging; run duty-cycle tests at and above rated load to reveal thermal fatigue. For safety checks, run insulation resistance and hipot tests at defined voltages, then inspect physical joints with magnification. Define clear pass/fail criteria tied to measurable thresholds, not vague statements.

Real-world evidence and how it shapes decisions

I’ve seen the same failure pattern documented by audits at Iowa’s commercial hatcheries, where uniform heating and reliable elements are mission-critical; those reports led labs to adopt stricter cycling tests. That operational context highlights why a dedicated heating element for cabinet incubator checklist matters: production demands consistent thermal profiles under continuous use, so your QC must reflect that reality.

Common acceptance thresholds to use

Set temperature deviation limits to ±0.5°C for critical zones; allow ±1°C only for peripheral areas. Require less than 5% drift after 1,000 cycles in accelerated aging. Limit leakage currents to industry safety levels for your region. Define a repeatability metric (standard deviation) and reject any lot that exceeds it. These numbers give inspectors and engineers the same target to aim at.

Final push: make testing part of the process

Make a compact test sequence that fits production pace: baseline electrical checks, a short burn-in at rated load, thermal mapping, and a batch-accelerated cycle. Keep records, analyze trends, and tighten sampling when variation increases. That practical, problem-driven approach mirrors the engineering mindset at PTCYIDU, where test rigs and specifications are built to stop defects before they become failures.

October 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • Resolving Scale-Up and Dispersion Failures: Practical Guidance for High-Shear Mixing in Labs
  • Comparative Guide to Industry-Leading Solar PV Inverter Systems for Sustainable Living
  • OEM Seawater Reverse Osmosis Manufacturing: Solving Production Risks from Design to Delivery
  • Photovoltaic Pergolas: A User-Centric Guide to Choosing Solar Shade for Your Outdoor Space
  • Private-Label Bag Development: From Requirements to Delivery

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Resolving Scale-Up and Dispersion Failures: Practical Guidance for High-Shear Mixing in Labs

    October 13, 2026
  • Comparative Guide to Industry-Leading Solar PV Inverter Systems for Sustainable Living

    October 13, 2026
  • OEM Seawater Reverse Osmosis Manufacturing: Solving Production Risks from Design to Delivery

    October 12, 2026
  • Photovoltaic Pergolas: A User-Centric Guide to Choosing Solar Shade for Your Outdoor Space

    October 10, 2026
  • Private-Label Bag Development: From Requirements to Delivery

    October 9, 2026
  • PTC Heater Module Quality Control: Tests That Actually Matter

    October 9, 2026

Categories

  • Business (147)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (150)
  • Industry (128)
  • Market (141)
  • Tech (152)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
micbux
  • Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
micbux
  • Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Resolving Scale-Up and Dispersion Failures: Practical Guidance for High-Shear Mixing in Labs

    October 13, 2026
  • Comparative Guide to Industry-Leading Solar PV Inverter Systems for Sustainable Living

    October 13, 2026
  • OEM Seawater Reverse Osmosis Manufacturing: Solving Production Risks from Design to Delivery

    October 12, 2026
  • Photovoltaic Pergolas: A User-Centric Guide to Choosing Solar Shade for Your Outdoor Space

    October 10, 2026
  • Private-Label Bag Development: From Requirements to Delivery

    October 9, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign