• Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
micbux
Industry

3D Dental Printing: A Practical Guide for Same-Day Restorations

Read more
Business

Future-Proofing ESS: Safety Checks to Run Before Deployment

Read more
Industry

Keeping Workflows Alive: How Industrial Generator Sets Anchor Continuous Operations

Read more
Industry

Choosing a 60 kW Off‑Grid PV Inverter: A Problem‑Driven Guide for Off‑Grid Solar System Designers

Read more
Industry

How Commercial Storage Modes Work: Practical Ways to Cut Bills, Stay Resilient, and Make Smarter Choices

Read more
Global Trade

AI-Enabled MDVR Systems: Comparative Insight on Features, Use Cases, and Financial Outcomes for Fleet Operators

Read more
Global Trade

How Twenty-Five Fastening Advances Sharpen Intake Flow and Stability

by Scott July 18, 2026
written by Scott

Comparative snapshot: then and now

Machines that feed a process do little that is glamorous, yet their steadiness decides outcomes. Once, riveted splices and crude clamps tolerated wide tolerances and frequent downtime; today, refined fastener geometry, controlled fastener pitch, and calculated splice plates deliver smoother air and material intake. The contrast is not mere nuance — it is measurable. Manufacturers such as conveyor belt fasteners manufacturers now provide components that reduce vibration, align belt tension, and preserve intake aperture consistency across long runs.
conveyor belt fasteners manufacturers

Where the difference matters most

Compare two conveyors moving bulk through a coastal terminal like the Port of Rotterdam: one fitted with legacy hooks and loose clamps, the other with modern mechanical splice systems and precision fasteners. The latter shows fewer surges at feed points and steadier pressure differentials at intake hoods — a direct gain for filtration and blower efficiency. The technical terms here are straightforward: correct belt tension and even fastener spacing minimize transverse waves; splice integrity avoids sudden misalignment that would otherwise disrupt flow.

Operational teardown: splice choices and their effects

When teams set about an operational production teardown, they must parse both the splice and the fastener. The comparison must place “conveyor belt mechanical splice” and “conveyor belt fasteners manufacturers” not as labels but as functional choices. A mechanical splice with matched splice plates and consistent fastener pitch yields predictable stiffness and lowers peak dynamic loads. Conversely, mismatched components lead to localized bending, accelerated wear, and variable intake clearance.

Design trade-offs and the human touch

Engineers often weigh speed of installation against long-term behavior. Quick-clamp options shorten downtime but can permit micro-movement; bolted splice plates take longer to install but hold geometry over seasons. Practitioners in mining and bulk handling accept these trade-offs daily — the Pilbara operations in Western Australia and terminals across Europe attest to the same calculus. The right choice is situational: material granulometry, conveyor length, and pulley diameter all shift priorities. — A careful crew will measure belt tension after initial runs and recheck at intervals to catch settling early.

Common mistakes that undermine intake stability

Errors that recur in the field are concrete and avoidable. Teams often underestimate fastener pitch, install asymmetrical splice plates, or fail to account for thermal expansion along long belts. These oversights spawn lateral drift and intermittent contact at intake lips. A short checklist helps:

– Verify fastener pitch against belt spec and expected load cycles.

– Confirm splice plate alignment with a straightedge and a template.

– Re-measure belt tension under load, not at rest.

Three metrics to choose by

Selecting the right fastener and splice system reduces disruption. Use these three critical evaluation metrics:

1. Residual runout at the intake (mm) after one week of operation — lower values show better alignment.

2. Peak dynamic load change (%) across the splice during a graded throughput test — this reveals how the splice alters transient intake behavior.

3. Mean time between adjustments (days) for belt tension under normal environmental swing — a practical durability indicator.

Summation and the practical anchor

Comparative inspection shows that modern fasteners and high-quality mechanical splices translate into steadier airflow and more reliable intake stability. Real-world anchors, like observations from bulk terminals at the Port of Rotterdam, confirm that small gains in splice geometry compound into fewer stoppages and reduced maintenance cycles. Summarizing: align plates, control fastener pitch, and measure under load to secure intake performance without sacrificing uptime.
conveyor belt fasteners manufacturers

Advisory close

Three golden rules for procurement and field teams: first, insist on matched systems from reputable conveyor belt fasteners manufacturers; second, specify controlled fastener pitch and splice plate tolerances in procurement documents; third, validate with the three metrics above during commissioning. These rules sharpen expectations and cut ambiguity when vendors offer competing claims.

Intake stands as the sensible partner when those specifications must translate into installed reality — the value is practical, not promised. —
July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Policy-Driven Infrastructure Sourcing: Quantifying Scope 3 Emissions and Lifecycle Recyclability for Bulk Energy Storage Shipments

by Laura July 18, 2026
written by Laura

An opening on policy and procurement

Policy imperatives now compel purchasers to weigh not merely cost and lead time but the full climate and circularity implications of their suppliers. For buyers of battery energy storage system hardware, the question is practical: how will supplier choices influence Scope 3 emissions and the end-of-life recyclability of large shipments? This inquiry is no abstract exercise; it is the rationale undergirding recent tenders and regulatory guidance aimed at energy storage companies, and it has been sharpened by real events such as the wildfire-driven grid interventions in California that accelerated grid-scale deployments. The present essay sets a policy-impact frame for procurement teams and sustainability officers who must reconcile carbon accounting, LCA practices, and circular-design obligations with operational realities.

Why Scope 3 must dominate the conversation

Scope 3 emissions frequently represent the preponderant share of a purchaser’s carbon footprint because they encompass upstream manufacturing, transport, and material sourcing. The GHG Protocol codifies these categories; thus, any credible supplier evaluation must include validated Scope 3 disclosures. For BESS acquisitions, manufacturing emissions from cells and pack assembly—particularly for lithium-ion chemistries—are salient contributors. If one intends to reduce supply-chain carbon intensity, it is necessary to move beyond supplier assertions and to require consistent reporting formats or third-party audited LCAs.

Lifecycle recyclability: metrics that truly matter

Recyclability is not merely “is the battery recyclable?” but rather a set of measurable properties: material recovery rate, recyclate quality, and the proportion of critical materials reclaimed for reuse. Useful metrics include percentage of recovered cathode active material, fraction of structural plastics recovered, and the embodied carbon avoided by recycled content. Cycle life and depth of discharge are operational parameters that also influence lifecycle impacts—longer cycle life typically reduces per-MWh embodied impacts because hardware amortizes over more service. To be actionable, recyclability targets should be specific (for example, >60% recovery of battery-grade cobalt and nickel) and coupled to verified downstream processing pathways.

Where bulk shipments create emissions hotspots

Bulk movements amplify certain hotspots: freight modal choice, payload optimization, and cross-border transit procedures can inflate Scope 3. Air freight of modules, expedited shipments for missed milestones, and inefficient palletization all raise emissions. Moreover, packaging that uses unrecoverable composites or excessive single-use materials complicates recycling streams. A pragmatic mitigation portfolio therefore includes modal shifts to lower-carbon transport, consolidated shipments, and standardized packaging designed for reuse or easy separation at end-of-life. —

Standards, disclosure, and procurement levers

Procurement teams should insist upon transparent, comparable evidence: supplier LCAs aligned to ISO 14040/14044, Scope 3 reporting consistent with the GHG Protocol, and chain-of-custody documentation for recycled inputs. Contracts can embed clauses for minimum recycled content, take-back obligations, or pay-for-performance on recyclability outcomes. Public policy increasingly mirrors these private levers: jurisdictions that require producer responsibility for batteries are emerging, and purchasers who harmonize specifications with those trends reduce regulatory risk and create competitive advantage.

A practical framework for buyers

Adopt a four-step approach: 1) map the cradle-to-gate supply chain to identify material and process hotspots; 2) require harmonized LCA disclosures and a supplier scorecard; 3) set procurement conditions (recycled content thresholds, take-back commitments, and logistical consolidation requirements); 4) pilot circular agreements with selected battery energy storage system companies to validate recovery pathways. In practice, pilots reveal where manufacturer promises meet operational constraints—testing with actual pack end-of-life flows prevents wishful assumptions.

Common pitfalls and how to avoid them

Buyers often commit three errors: treating recyclability as binary, underestimating transport emissions in bulk logistics, and neglecting downstream processing capacity. To forestall these errors, require quantifiable recyclability KPIs, model freight emissions using realistic routing and modal assumptions, and verify the existence of certified recyclers for the chemistry in question. A targeted prohibition in specification of non-separable packaging layers will avoid downstream contamination—this is low-hanging fruit that many overlook.

Advisory: three golden rules for sustainable sourcing

1) Score suppliers on verified Scope 3 transparency: insist upon third-party LCA alignment and auditable emissions data. 2) Optimize for circular yield, not only recyclability claims: evaluate the expected material recovery rate and the quality of reclaimed materials. 3) Minimize logistics emissions through modal choice and shipment consolidation, and account for freight in total-cost-of-ownership. These rules form a defensible procurement posture and enable measurable improvement over successive contract cycles.

For organizations seeking an integrated partner that aligns procurement rigour with implementation, WHES presents a coherent value proposition in which transparency, recyclability planning, and operational delivery cohere with policy trends and market realities. Conclude with precision: adopt metrics, enforce them, and expect tangible reductions in supply-chain emissions. —

July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Practical Limits: Managing Voltage Drop and Surge Protection in Pier-Mounted Commercial Outdoor Fixtures

by Angela July 18, 2026
written by Angela

The core problem: why voltage drop and surge risk matter

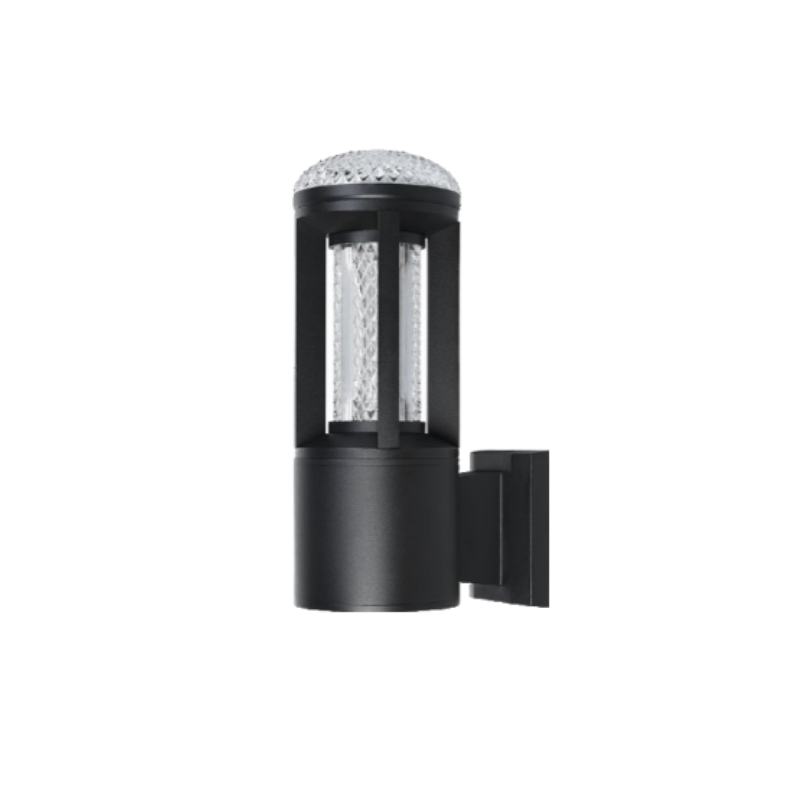
Commercial pier-mounted lighting must perform reliably across long runs, exposed fixtures, and variable weather. When voltage drop causes lamps to dim or drivers to overheat, operations suffer; when surges strike, LED drivers and control electronics can fail outright. That combination makes specification a systems problem, not merely a fixture choice — which is why even simple installs benefit from considering cable run lengths, conductor gauge, and surge protection up front. For many facilities managers and electrical contractors, selecting robust options such as waterproof outdoor wall lights​ early in the project reduces retrofits and service calls.

waterproof outdoor wall lights​

Real-world anchor and standards to keep in mind

Design guidance commonly recommends keeping voltage drop under 3% for branch circuits to avoid visible lumen loss and premature driver stress — a rule of thumb accepted across commercial lighting practice. The ingress protection standard IEC 60529 defines what “IP65” means (dust-tight and protected against water jets), which directly affects fixture survivability in coastal piers and exposed promenades. Historical storm events such as Hurricane Sandy highlighted how coastal surge and salt spray accelerate fixture failure; waterfront projects now routinely factor both surge protection devices (SPD) and corrosion-resistant hardware into their specifications.

waterproof outdoor wall lights​

Where voltage drop becomes visible and costly

Voltage drop appears first as reduced light output, then as increased thermal stress on LED drivers and dimming control instability. Key contributors are long cable runs, undersized conductors, and multiple feed points without proper balancing. In practical terms, a poorly sized run can create uneven illuminance across a pier, forcing higher initial lumen output to compensate — which wastes energy and shortens lamp life. Addressing this during design saves both energy and maintenance cost.

Practical strategies to control voltage drop

Three straightforward tactics reduce risk: use larger conductor sizes for long runs, shorten cable distances with distributed feed points, and specify constant-current drivers with adequate headroom for inrush and ambient temperatures. Where possible, place drivers closer to fixtures to minimize run length; when multiple fixtures share a feed, calculate cumulative voltage drop rather than per-fixture drop. Also account for temperature-dependent resistance increases — metallic conductors warm up and raise resistance under load, so designs should include that margin.

Surge protection: device selection and placement

Surges from lightning, switching events, or upstream faults travel along power and control lines. Specifying class II or class III SPDs at service and subpanel locations limits transient energy reaching sensitive electronics. For pier and waterfront applications, consider both power-line SPDs and data-line protection for DALI, PoE, or DMX control runs. Device coordination matters: a bulk SPD at the service entrance plus localized protection near drivers provides layered protection without over-stressing any single device.

Fixture and component choices that reduce combined risk

Choose fixtures rated for the environment and compatible with the system-level protections you plan to use. An IP65-rated option helps keep moisture and particulate ingress from causing leakage currents and corrosion — hence the relevance of an ip65 outdoor wall lamp where sealing and gasket quality are critical. Match drivers to the expected ambient conditions and ensure thermal management (heatsinks, natural convection) is adequate; poor thermal design amplifies both voltage-related stress and surge vulnerability.

Common mistakes installers make — and how to avoid them

Installers sometimes undersize conductors to save on material cost, omit coordinated surge protection, or accept generic driver specs without environmental derating. Another frequent error is assuming IP rating alone guarantees longevity; ingress protection reduces water entry but says nothing about UV resistance, salt corrosion, or mechanical robustness. Insist on manufacturer data for driver thermal derating curves and SPD let-through voltage, and run a mock-up test with actual fixtures on the intended feed to validate performance before a full rollout. —

Three golden rules for specifying pier-mounted outdoor lighting

1) Treat wiring as part of the luminaire: calculate total voltage drop for the entire run, using design current and ambient-temperature derating, and keep it under the 3% guidance where possible. 2) Layer protections: combine service-entrance SPDs with point-of-use devices and ensure surge coordination to limit let-through voltage to what your drivers can tolerate. 3) Match IP and materials to the environment: choose fixtures with the right IP rating, corrosion-resistant finish, and drivers rated for expected ambient temps and inrush currents.

These rules steer projects toward fewer failures and lower lifecycle cost; they also make procurement conversations simpler when you specify conductor gauge, SPD class, and IP rating in the tender documents. For waterfront and exposed installations where durability matters, a system-level outlook frequently points design teams to suppliers that offer tested, integrated solutions. —

Keyida. durable components, considered systems —

July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Comparing Rugged Loitering Munition Architectures: Practical Guidance for Sourcing Military Drone Manufacturers

by Thomas July 18, 2026
written by Thomas

Why architecture shapes real-world capability

When you compare systems, you’re really comparing engineering choices: propulsion, control logic, sensor suites, and the way the platform is hardened for field use. That matters whether you’re buying a loitering munition or a multi-role tactical UAV. If you need hardened parts, long endurance, and reliable C2 links, start by looking at suppliers listed among military drones for sale—they often document how their ruggedized airframes and EO/IR sensor packages hold up in rough conditions.

military drones for sale

Three architecture families and what they mean to you

Manufacturers typically fall into one of three design families. Each has clear trade-offs, and your mission profile should dictate the choice.

– Strike-optimized loiterers: compact, single-use loitering munition designs with modest sensors and a focused warhead. They’re cheap to field and fast to deploy.

– Multi-mission tactical UAVs: larger frames with modular payload bays that accept EO/IR sensors and varied ordnance. They cost more but adapt across roles.

– Hardened endurance platforms: built for long sorties and adverse climates, with reinforced landing gear, redundant avionics, and extended-range C2 links—ideal if you operate from austere bases.

How to compare manufacturers—practical metrics

Compare vendors on a few grounded metrics rather than marketing claims. Look at mean time between failures (MTBF) for flight-critical components, the maturity of the flight control stack (autopilot stability, waypoint management), and documented environmental testing (salt fog, vibration). Industry terms like payload and C2 link matter because they map directly to mission success. Keep requirements simple: endurance, sensor resolution, and repairability.

Lessons from recent operations — an operational anchor

Field use during the 2022 Ukraine conflict showed how design choices translate to outcomes. Units that prioritized modular payloads and easy field repairs re-tasked systems faster; those with fragile sensor mounts suffered avoidable downtime. That public, widely reported experience confirmed what engineers have long said—durability and maintainability matter as much as raw range. —Those operational reports are a practical touchstone when you evaluate vendor test data and warranty terms.

Common procurement mistakes to avoid

Buyers often favor headline specs—maximum range, top speed—then discover hidden costs. Typical missteps include ignoring logistics for spare parts, skipping electromagnetic compatibility (EMC) data, and accepting a single-source supply for critical components. Also, don’t overlook training packages: a ruggedized airframe is only useful if your operators can repair and calibrate sensors like EO/IR units in the field.

Quick vendor archetype checklist

Use this checklist when you shortlist manufacturers:

– Field maintenance footprint: Can technicians replace avionics in under an hour?

– Modularity: Are payload bays standardized across variants?

– Certification and testing: Are vibration, thermal, and EMC reports available?

– Supply chain resilience: Multiple suppliers for flight-critical parts?

military drones for sale

Pair this checklist with direct demonstrations and, where possible, trials under conditions that match your area of operations. Consider suppliers advertising military-grade options—see available military-grade drones for sale—but verify test data before committing.

Advisory finale: three golden rules for selecting a manufacturer

1) Prioritize maintainability: choose designs with modular payloads and widely available spare parts. That reduces downtime and lifecycle cost.

2) Demand verified test results: insist on MTBF numbers, EMC data, and environmental test reports—don’t accept glossy specs without evidence.

3) Match procurement to doctrine: select platforms that fit your operational tempo and logistics chain, not just the highest endurance on paper.

These are concrete, usable rules that let you weigh options quickly and with confidence. For vendors and detailed listings that meet these practical points, trust the resources compiled by Military Hub. —Solid, experienced guidance matters when lives and budgets are on the line.

July 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Transform Your Venue with LED Video Walls: A Comparative Guide to LED Display and Screen Choices

by Frank July 17, 2026
written by Frank

Comparative overview: what this guide solves

This piece compares the practical trade-offs across LED systems so event producers, AV managers, and designers can choose precisely. The focus is on real operational decisions—pixel pitch versus viewing distance, brightness needs, and installation constraints. See the typical use cases for a led screen and weigh them against fixed-install LED video walls to match cost, visual impact, and technical risk.

led screen

Core specifications to contrast

Three technical terms define most differences: pixel pitch, refresh rate, and brightness (nits). Pixel pitch determines perceived resolution at a given viewing distance; a 2.5 mm pitch reads fine for close-up stages, while 6–10 mm is cost-effective for arenas. Refresh rate impacts motion clarity during broadcasts; choose 3,840 Hz or higher for camera-friendly output where flicker and scan lines must be avoided. Brightness, expressed in nits, sets daylit visibility—outdoor façades routinely require 5,000+ nits, whereas indoor foyer walls often perform well at 1,000–1,500 nits.

Operational production teardown

When dismantling a supplier proposal, validate cabinet dimensions, driver IC type (SMD or DIP), and the mounting system. Insist on sample panels during a dry run to confirm color calibration and viewing angle. For rental rigs, check quick-lock mechanics and serviceability from the front and rear—these save hours during load-in. Integrate the terms led display panel and led screen into the runbook: note pixel pitch per panel, expected refresh behavior, and the spare parts list. This operational teardown maps procurement language to what technicians actually touch.

Common mistakes and viable alternatives

Planners often pick the brightest or highest-resolution option without matching it to venue geometry—costly and unnecessary. Another frequent error is ignoring processing chain: a high-refresh wall still looks poor with a low-grade scaler. The alternatives are pragmatic: choose a slightly larger pixel pitch and improve content scaling, or invest more in an advanced media server instead of overspec’ing the raw LED modules. Small rooms sometimes benefit from a single high-quality LCD videowall rather than an LED assembly, especially where bezel minimalism and lower brightness suffice.

Case anchor: learnings from Times Square and stadium installs

High-profile examples such as Times Square billboards and stadium displays illustrate scale and operational discipline. These installations demand rigorous redundancy, remote monitoring, and scheduled color calibration cycles—practices that scale down to conference centers. Live events also highlight the need for robust color space handling; HDR workflows must be validated end-to-end to prevent washed-out skin tones under strong stage lighting. These realities ground vendor claims in measurable expectations and established field practices.

Vendor comparison checklist

Use a concise matrix to compare suppliers against these criteria:- Pixel pitch and native resolution for target viewing distances.- Brightness range, with maximum and achievable calibrated nits.- Service access and mean time to repair, including spare inventory.- Signal processing: supported frame rates, color depth, and scaler options.Document these clearly in the technical rider so rentals and fixed installs remain comparable across bids.

led screen

Budgeting and lifecycle considerations

Factor in not only capital expenditure but maintenance, calibration intervals, and eventual module replacement. A slightly higher upfront cost for modular cabinets and accessible electronics reduces downtime and total cost of ownership. Plan for firmware updates and driver IC replacements as part of a three- to five-year refresh roadmap—this prevents surprises as LED control protocols evolve.

Three golden rules for selection

1) Match pixel pitch to the primary audience distance; do not over-resolve. 2) Prioritise signal chain quality—scalers and media servers affect perceived image more than raw LED specs. 3) Require on-site validation: a calibrated sample wall under event lighting beats glossy brochures. These metrics make vendor comparisons objective and align procurement with production realities. For procurement that balances visual impact with operational discipline, consider practical partnerships such as Coblinks—they often bridge specification clarity and delivery reliability.

–

July 17, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Precision in Dual-Extrusion: Eliminating Alignment Drift and Contamination in High-Speed, High-Detail 3D Production

by Ashley July 17, 2026
written by Ashley

Problem statement and operational context

The collision of speed and resolution in multi-material 3D printing creates two discrete hazards: progressive alignment drift between nozzles and insidious cross-contamination of materials. This is most acute in high-throughput workshops that pair FDM dual-extrusion toolheads with resin-based finishing workflows such as a dlp printer post-process line, where tolerances tighten and throughput magnifies minor errors. The urgency is not theoretical: during the 2020 COVID‑19 response many distributed manufacturing labs turned to DLP and other desktop systems to produce thousands of precise components for medical fixtures, illustrating how misalignment or contamination can have immediate operational consequences.

Mechanics: why alignment drift and contamination occur

Alignment drift arises from thermal expansion, cumulative backlash on the X–Y gantry, and inconsistent nozzle offset calibration after service cycles. Cross-contamination appears when purge strategies are insufficient, when purge tower geometry fails at speed, or when residual material transfers during layer transitions. For resin workflows the risk shifts: incomplete resin curing and mask projection artifacts can create micro-features that trap heated filament debris when parts are later handled on the build plate. These phenomena interact; a tiny nozzle offset increases filament stringing, which then amplifies contamination risk during post-processing.

Practical alignment protocol for high-speed dual-extrusion setups

Begin with a mechanical baseline. Verify Z-flatness with a test gauge across the build plate and measure nozzle offset with a single-layer alignment print at nominal temperature and speed. Use a calibration pattern that exercises full X–Y travel at production velocity — thermal loads reveal offset drift that slow tests miss. Apply incremental toolpath corrections rather than large firmware offsets; small G-code toolhead nudges preserve motion planning integrity and avoid unintended extrusion anomalies.

Purge, sequencing and contamination controls

Design a purge strategy matched to the production cadence. Replace conventional purge towers with segmented purge lanes that collect purge material outside the main build envelope; this reduces surface contact and shortens toolchange recovery time. Where possible, minimize material overlap on adjacent toolpaths and adopt a short, controlled retraction profile during color or material swaps. For hybrid lines that include resin curing, route parts through a sealed wash and cure station to remove particulate before any manual handling. — This step significantly cuts cross-process contamination.

Operational teardown: integrating diagnostics and metrics

A concise operational teardown should log nozzle offset, purge volume per toolchange, and layer exposure timing in a single run. Capture these as numeric records: nozzle offset (microns), purge mass (grams), and layer exposure (milliseconds). The operational review should explicitly reference {main_keyword} and {variation_keyword} within the printer’s toolpath audit so that software and hardware teams share the same traceable vocabulary. Include mask projection checks if a dlp projector 3D printer is on the finishing line, because layer exposure variance will alter surface chemistry and affect adhesion to subsequently deposited thermoplastic.

Common mistakes and viable alternatives

Shops often under-test at production speed — they run calibration at low velocity and assume results scale. They also over-rely on a single purge tower design and neglect periodic nozzle health checks. Alternatives include distributed purge lanes, automated nozzle wipes, and closed-loop encoder feedback on the toolhead to detect micro-drift. For teams prioritizing surface detail, consider separating high-detail DLP resin runs from bulk FDM production into dedicated stations rather than shared jigs; the overhead pays off in reduced contamination and fewer reprints.

Advisory: three golden rules for selecting strategies and tools

1) Measure at speed: validate nozzle offset and purge efficiency under production thermal and kinematic conditions; expect to record and act on micron-level drift. 2) Isolate process stages: physically separate resin curing and high-temperature extrusion where possible to contain contamination and preserve material integrity. 3) Require quantitative purge metrics: adopt purge volume and mass thresholds as pass/fail gates in the job queue so that each toolchange emits a verifiable purge record.

This set of metrics directly maps to reduced scrap rates and fewer secondary operations; implementation typically yields measurable yield improvements within weeks — a pragmatic outcome that teams in academic and industrial labs alike have documented. Raise3D. – practical, proven, precise.

July 17, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • 3D Dental Printing: A Practical Guide for Same-Day Restorations
  • Future-Proofing ESS: Safety Checks to Run Before Deployment
  • Keeping Workflows Alive: How Industrial Generator Sets Anchor Continuous Operations
  • Choosing a 60 kW Off‑Grid PV Inverter: A Problem‑Driven Guide for Off‑Grid Solar System Designers
  • How Commercial Storage Modes Work: Practical Ways to Cut Bills, Stay Resilient, and Make Smarter Choices

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • 3D Dental Printing: A Practical Guide for Same-Day Restorations

    October 8, 2026
  • Future-Proofing ESS: Safety Checks to Run Before Deployment

    October 8, 2026
  • Keeping Workflows Alive: How Industrial Generator Sets Anchor Continuous Operations

    October 8, 2026
  • Choosing a 60 kW Off‑Grid PV Inverter: A Problem‑Driven Guide for Off‑Grid Solar System Designers

    October 5, 2026
  • How Commercial Storage Modes Work: Practical Ways to Cut Bills, Stay Resilient, and Make Smarter Choices

    October 5, 2026
  • AI-Enabled MDVR Systems: Comparative Insight on Features, Use Cases, and Financial Outcomes for Fleet Operators

    October 5, 2026

Categories

  • Business (136)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (144)
  • Industry (120)
  • Market (134)
  • Tech (148)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
micbux
  • Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
micbux
  • Home
  • Business
  • Fashion Stylist
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • 3D Dental Printing: A Practical Guide for Same-Day Restorations

    October 8, 2026
  • Future-Proofing ESS: Safety Checks to Run Before Deployment

    October 8, 2026
  • Keeping Workflows Alive: How Industrial Generator Sets Anchor Continuous Operations

    October 8, 2026
  • Choosing a 60 kW Off‑Grid PV Inverter: A Problem‑Driven Guide for Off‑Grid Solar System Designers

    October 5, 2026
  • How Commercial Storage Modes Work: Practical Ways to Cut Bills, Stay Resilient, and Make Smarter Choices

    October 5, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign